Pallet Conveyors
Engineered for weight, these lines move heavy pallet loads safely between storage, production, and automated equipment.
Why Choose Pallet Conveyors
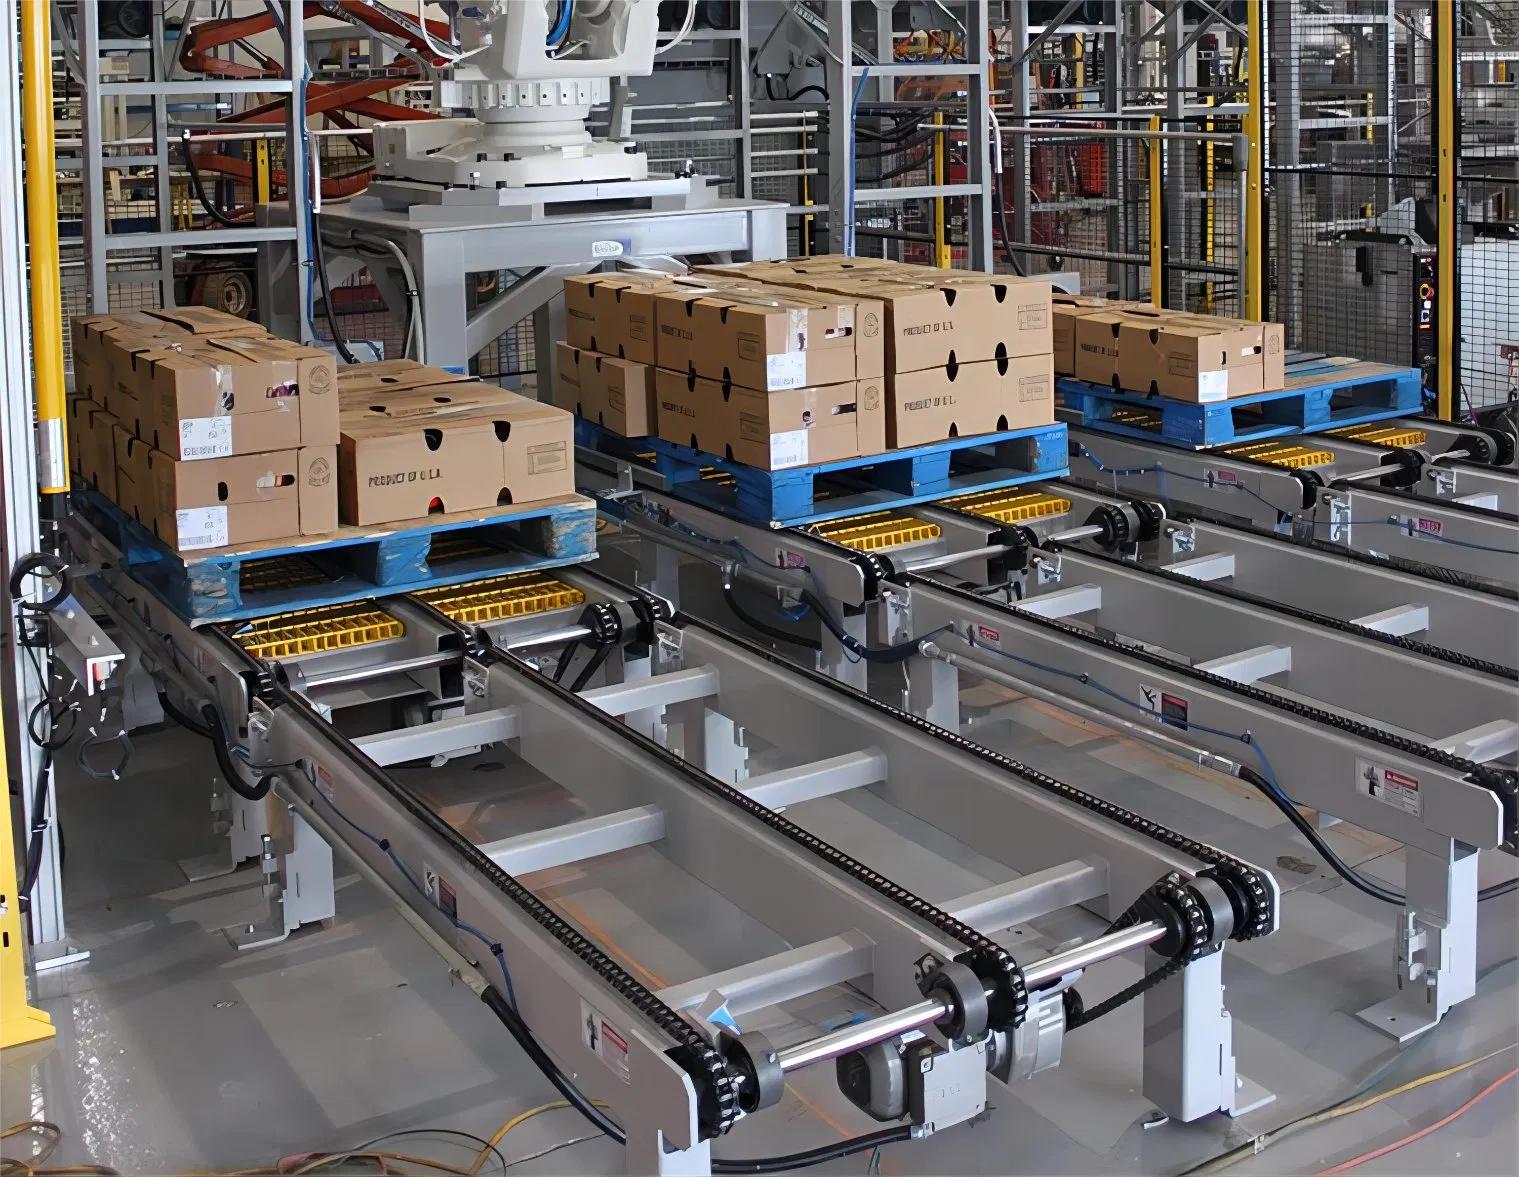
Pallet conveyor is built to a different weight class than carton or tote lines—heavier rollers or chain-driven decks, reinforced frames, and drive systems sized to move full pallet loads safely and consistently between storage, production, and automated equipment.
It shows up wherever pallets need to move without a forklift in the loop—feeding AS/RS systems, palletizers, stretch wrappers, and staging lanes—and it's often the physical connection point between storage systems and automation equipment in a facility.
Is Pallet Conveyors Right for Your Facility?
Best fit: Heavy, automated pallet movement.
Talk with us about your layout, throughput, and equipment before locking in a system—we'll help confirm whether this is the right call or whether another approach fits better.
Key Advantages
- Built to full pallet load ratings, not carton or tote weights
- Chain-driven and roller options depending on load and speed
- Common link between storage, palletizing, and wrapping equipment
- Feeds AS/RS and other automated storage systems directly
- Reduces forklift traffic in production and staging areas
More Conveyors & Transport
Ready to Talk Through Pallet Conveyors?
Tell us about your facility and we'll help you figure out if this is the right system for how you operate.